How Does Stick Welding Work?
How does stick welding work? Find out what you can weld with a stick welder and if MIG welding is stronger than stick welding?
What is Stick Welding?
Stick welding, also known as Shielded Metal Arc Welding (SMAW), is one of the most commonly used techniques across all arc welding processes. It uses an electric current and an anode at the weld pool to join together various types of metal, from copper to steel.
Stick Welding is a very versatile technique, with it dating back to 1889 when Charles L. Coffin patented the arc welding process using a metal electrode. The technique remains a popular choice today, with many beginners taking on this method first.
Stick welding is mainly used for welding iron or steel, and it is utilised widely in maintenance and repair industries. Stick welding can be completed outdoors and isn't affected by the wind like TIG or MIG, as it doesn't require a gas cylinder. This flexibility makes stick welding a popular choice amongst farmers and other outdoor industries. T's are also used for the construction of large, heavy steel structures.
How does it work?
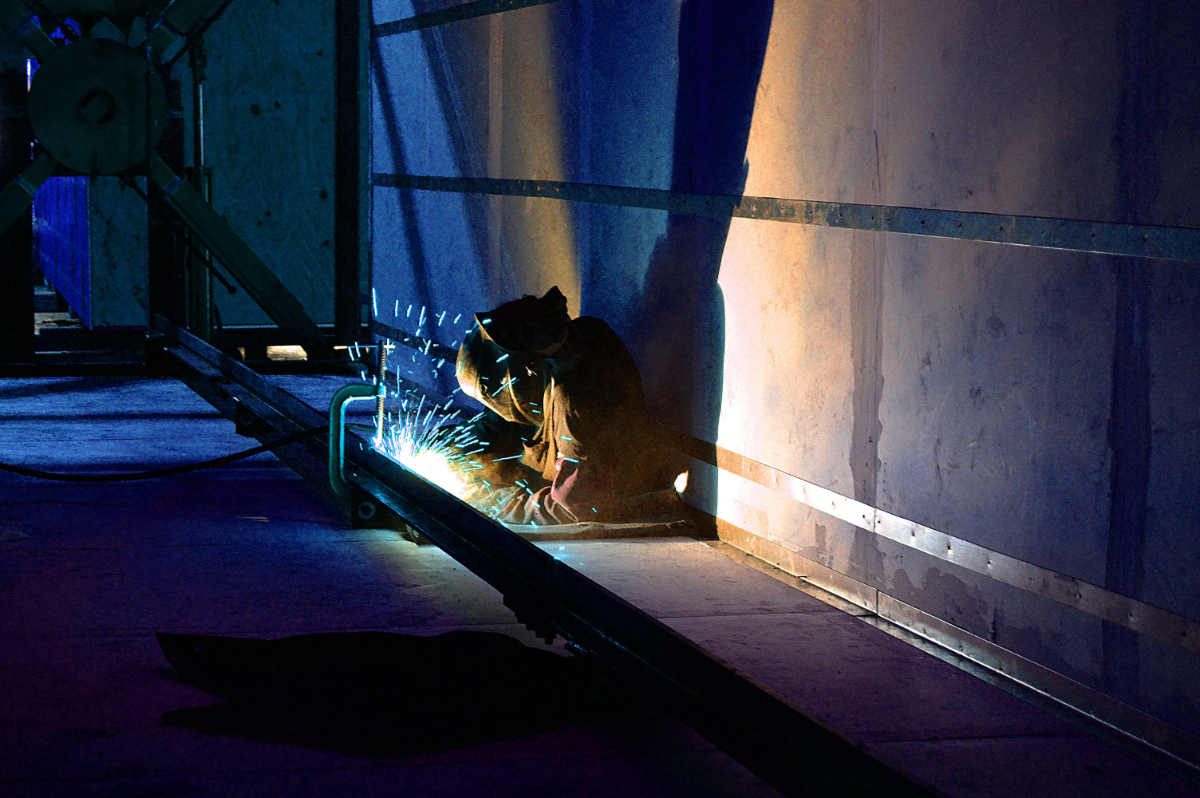
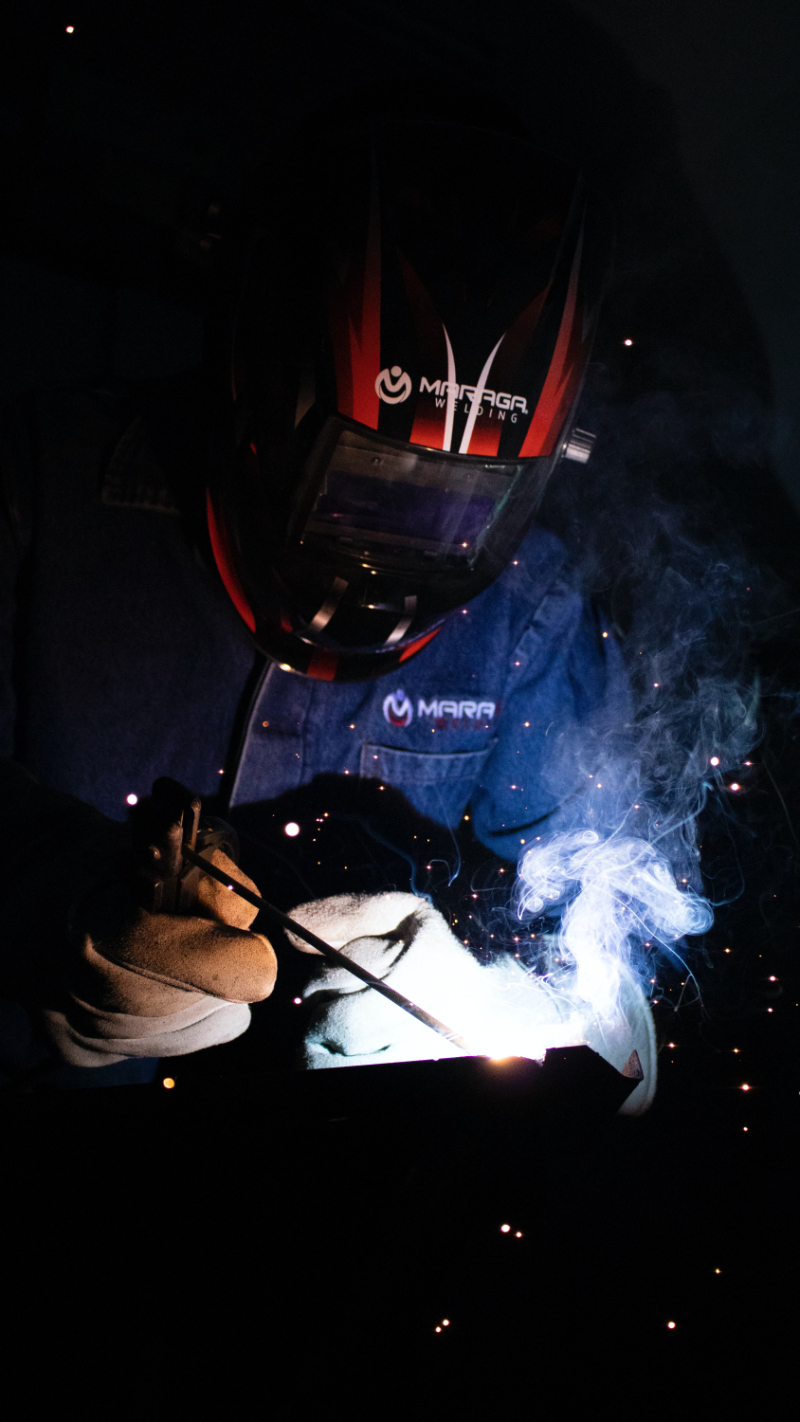
An electric arc forms between a flux-coated consumable electrode and the workpiece. It melts the electrode core and joint edges. The coating supplies shielding gases and forms slag that protects the cooling weld.
An electric current (AC or DC) produces the electric arc between the metal material and the electrode (rod). The spot between the two is known as the weld pool, as this is where the metal liquifies.
What Can I Weld with a Stick Welder?
Stick welding is one of the most versatile and widely used welding techniques for both maintenance and production welding.
This welding technique can also be applied in ALL welding positions (flat, vertical, horizontal, overhead and pipe & groove), as well as being applicable for all ferrous metals.
Ferrous metals are known to have Iron in their makeup; most commonly, when using the name 'Ferrous', it comprises high volumes of Iron.
Although stick welding has various multi-uses, it works best with thicker metals and performance the least well with thinner sheet metal.
If you are working with a sheet metal that is 1/15 or thinner, then a TIG or MIG weld would be a better choice than Shielded Metal Arc Welding (SMAW).
Nevertheless, some of stick welding's best uses include; Fixing Farm Equipment, Tractor Repairs, Ship construction, Power Plant construction and Structural Steel.
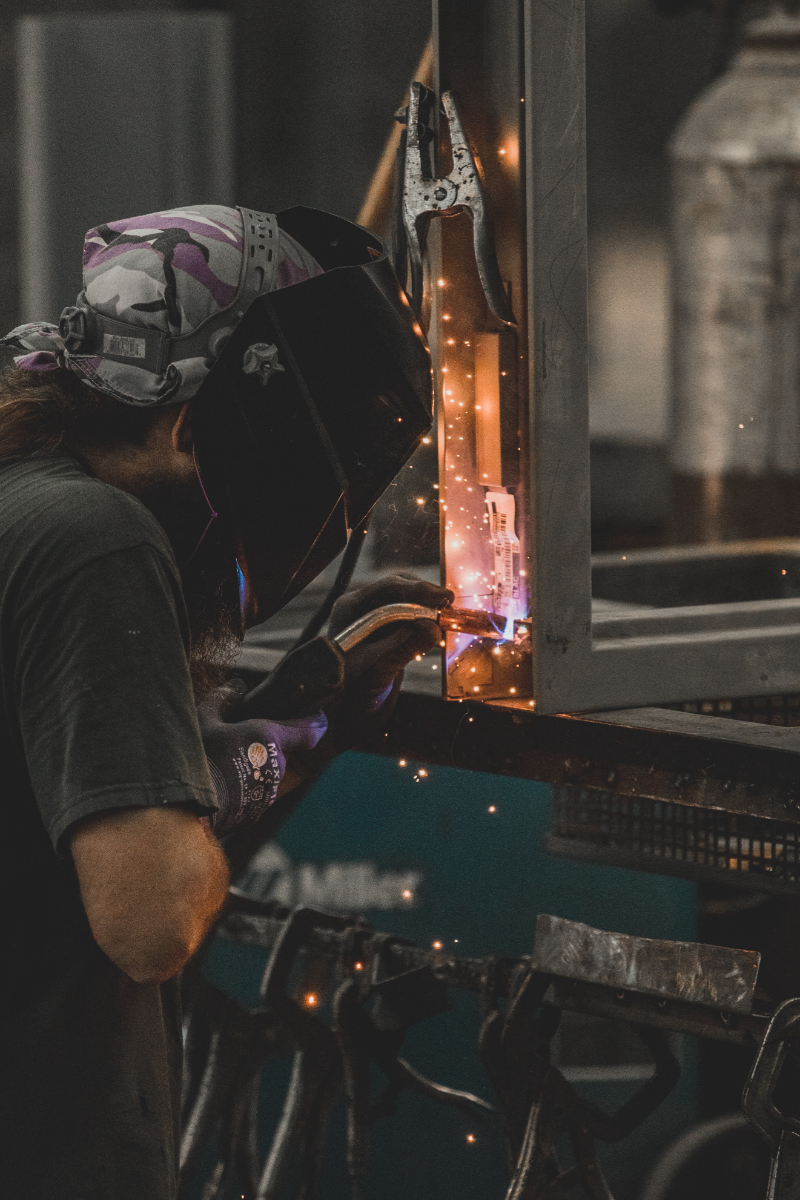
As discussed, Stick welding is one of the most versatile welding methods available that is applicable for a variety of metal types, including Ferrous metals (very high in iron). The wide range of metals you can use the stick weld technique on include;
- Steel
- Stainless steel
- Nickel-based alloys
- Chrome
- Stainless steel to regular steel
- Aluminium (not ideal)
Push Or Pull: Stick Welding.
Stick welding produces slag, which must be removed after each pass. For flat and horizontal work a drag technique is commonly used; vertical-up welding needs a different approach. Follow the electrode manufacturer’s guidance and welding procedure.
Is Stick Welding Easy To Learn?
Shielded Metal Arc Welding (SMAW) isn't the easiest welding technique for beginners to learn; however, it is the most versatile and, therefore, most valuable for home DIY enthusiasts, farmers and other construction industries.
It's relatively easy to teach the stick welding method, yet mastering the technique can take a longer time, a lot of knowledge and practice. However, if you choose to learn Stick Welding, we give some top pointers below to ensure your set-up is correct and begin to master the technique.
Electrode Selection
Select AC or DC and electrode polarity as specified for the rod. An anode is positive; the electrode is not always the anode. Current also depends on diameter, position and joint.
Arc Length
Having the right arc length is vital in stick welding. The arc length should be no more than the diameter of the electrode, with each application requiring a distinct length.
For instance, a 0.125 inch 6010 anode will need approximately 1/8 from the workpiece material.
Travel Angel
Always make sure the electrode is at the correct angle with your weld joint. When welding in an overhead or lying position, you can use a pull or backhand welding technique.
The electrode tip should be inclined 5-15°degrees toward the travel direction. When welding in a vertical position, use a push or forehand technique to travel upwards, and aim to slant the electrode at a 15°degree angle away from the travel direction.
Below we compare the Stick welding technique with TIG welding and MIG welding, breaking down which is easier, and the level of knowledge needed for each welding process.
TIG vs Stick Welding
Both TIG and Stick welds use a fusion welding process. Stick welding, however, is much easier and more versatile than TIG welding- owing to the complexity of the TIG process.
TIG welds are intended for professional high-precision welding tasks, meaning TIG welding requires more knowledge, training and experience and therefore takes much longer to master.
Stick welding equipment is also relatively inexpensive compared to TIG welding tools. Furthermore, stick welding can be carried out on rusted, dirty and painted metal surfaces, unlike TIG or MIG.
MIG vs Stick Welding
Firstly, Stick welding has been around for a much longer time than MIG, meaning many choose to master the universal welding technique (STICK) instead of the more recent method (MIG). However, MIG welding is the easier-to-learn technique after a slightly complex set-up of the equipment.
The set-up for MIG welding comprises wire size, wire type, contact tips, inert gas choice and nozzle type.Yet, once set up, MIG welding is incredibly easy and is often referred to as the "hot glue gun of welding" with a simple point-and-shoot approach.
Whatsmore, with MIG, there is less post-weld cleaning required, thanks to the smooth, slag-free and almost splatter-free welds. MIG welding is best used when assembling or creating advanced machinery inside workshops, away from the wind, generally working with clean and unpainted pieces of metal.
Although the moveability of Stick welding does overshadow MIG welding, thanks to the A/C or A/C-D/C powered machines. This is a big advantage for farmers with large acres to work across and small-time DIYers. If you need to work outside in the wind and have a portable welding machine, then Stick welding would be the right choice!
POWER: AC or DC
Stick welding is polarity driven, meaning it involves both positive and negative charges, along with magnetic or electrical poles.
Generally, stick welding will use Direct Current (DC) owing to its multiple advantages over Alertantin Current (AC). AC is typically used as a second option and only when necessary.
DC offers a more stable and smoother arc, fewer arc outages, less splatter, easier start-up and easier overhead/vertical welding.
DC's current supplies a deeper level of penetration and consistent current but has a higher deposition rate. A DC power supply may be preferred when working with thinner sheet metals to avoid a burn-out from deeper than needed penetration.
AC polarity is half DC positive and half DC negative.
Professional welders in the industry recommend sticking with DC power as it provides all the benefits of DC negative and DC positive whilst continuing to deliver a constant current. However, there are some cases where an AC polarity is used during welding. The most obvious reason is that only an AC output power supply is available; this issue is commonly seen with 'buzz box' welding machines, which are generally low-cost and entry-level machines for beginners.
How Does Stick Welding Work?
Like any other welding technique, with Shielded Metal Arc Welding (SMAW), you should first hook up the welding rod holder and the ground clamp to the power supply.
Next, hook the ground clamp up from the welder to the metal material. Lastly, place the welding rod in the electrode holder, and strike the workpiece surface where you want to start welding. Once the electrode starts to burn and deposit metal into the joint, the welding process has begun.
This process occurs when electricity is passed from the welder through the rod/electrode and arcs; contact then creates a temperature of 7,000° F or more! At this temperature, the rod/electrode starts to melt, along with the rods' coating forming a shield from external contaminations such as Oxygen.
This welding method is why stick welding is called SMAW/shielded metal arc welding because the shield around the electrode is what arches. Metal material continues to melt as you move the electrode along the joint, by first creating a crater and then filling it with liquified metal.
Simply, an electric current flows from the rod/electrode and meets the workpiece metal. Whilst the flux at the end of the rod creates a protective bubble between the metal being welded and the anode.
Choosing a stick welding electrode
The electrode is both filler metal and a source of shielding. Its coating breaks down during welding, producing protective gases and a slag layer. Choose a rod intended for the parent material, welding position and service conditions; different coatings change arc behaviour and handling.
Check the data sheet for permitted polarity, current range and storage instructions. Low-hydrogen electrodes need controlled storage and handling to preserve their intended properties. Rods with damaged coatings or moisture contamination should not be treated as equivalent to sound consumables. Diameter must suit the joint and machine output.
Controlling current and arc length
Use the electrode maker’s range as the starting point. Too little current can make the rod stick or leave poor fusion; too much can create excessive spatter and undercut. Move the holder towards the work as the rod shortens, maintaining the arc rather than stretching it.
Miller’s current stick welding technique guide recommends tuning current in steps of 5–10 amps. It gives a general arc-length starting limit of the electrode’s metal-core diameter. Both depend on the electrode and application; no single amperage suits every rod or position.
Preparing joints and removing slag between passes
Remove oil, paint, loose rust and other contamination before welding. Stick welding may tolerate some surface conditions better than solid-wire MIG, but welding over coatings can produce hazardous fume and compromise the joint.
- Prepare edges and root gaps to the required procedure.
- Attach the work return clamp to clean metal.
- Remove slag and inspect each pass before depositing the next.
- Check for cracks, undercut and trapped slag.
Neither MIG nor stick is automatically stronger. Joint design, filler compatibility, fusion and defects determine performance; critical repairs need the appropriate procedure and inspection.
Stick welding fume and outdoor work
Figures checked on 14 October 2026: HSE estimates around 11,000 lung disease deaths annually in Great Britain from past workplace exposures. This covers all occupational exposures, not welding alone, and reflects conditions years earlier.
Working outside does not remove the fume risk. HSE advises suitable RPE for outdoor welding, with protection for others nearby. Indoors, control fume at source. Wear eye protection when chipping slag and keep hot fragments away from people and combustible materials.
Are you looking for stick welding equipment suppliers in Coventry and Warwickshire. Contact our welding equipment specialists working across Coventry, Rugby, Oxford and the surrounding areas.